ALSONSHARDWARE
Drum Shaft Chroming for Drum Spindle
Client SectorIndustrial Rotary Drum & Mill Process Operators
Site LocationPrecision Machine Workshop & Hard Chrome Facility, Karachi
Turnaround Duration10 Days Turnkey
Quality VerificationCertified Handover
1 / 6
Technical Authority // Field Context
Project Scope & Operational Context
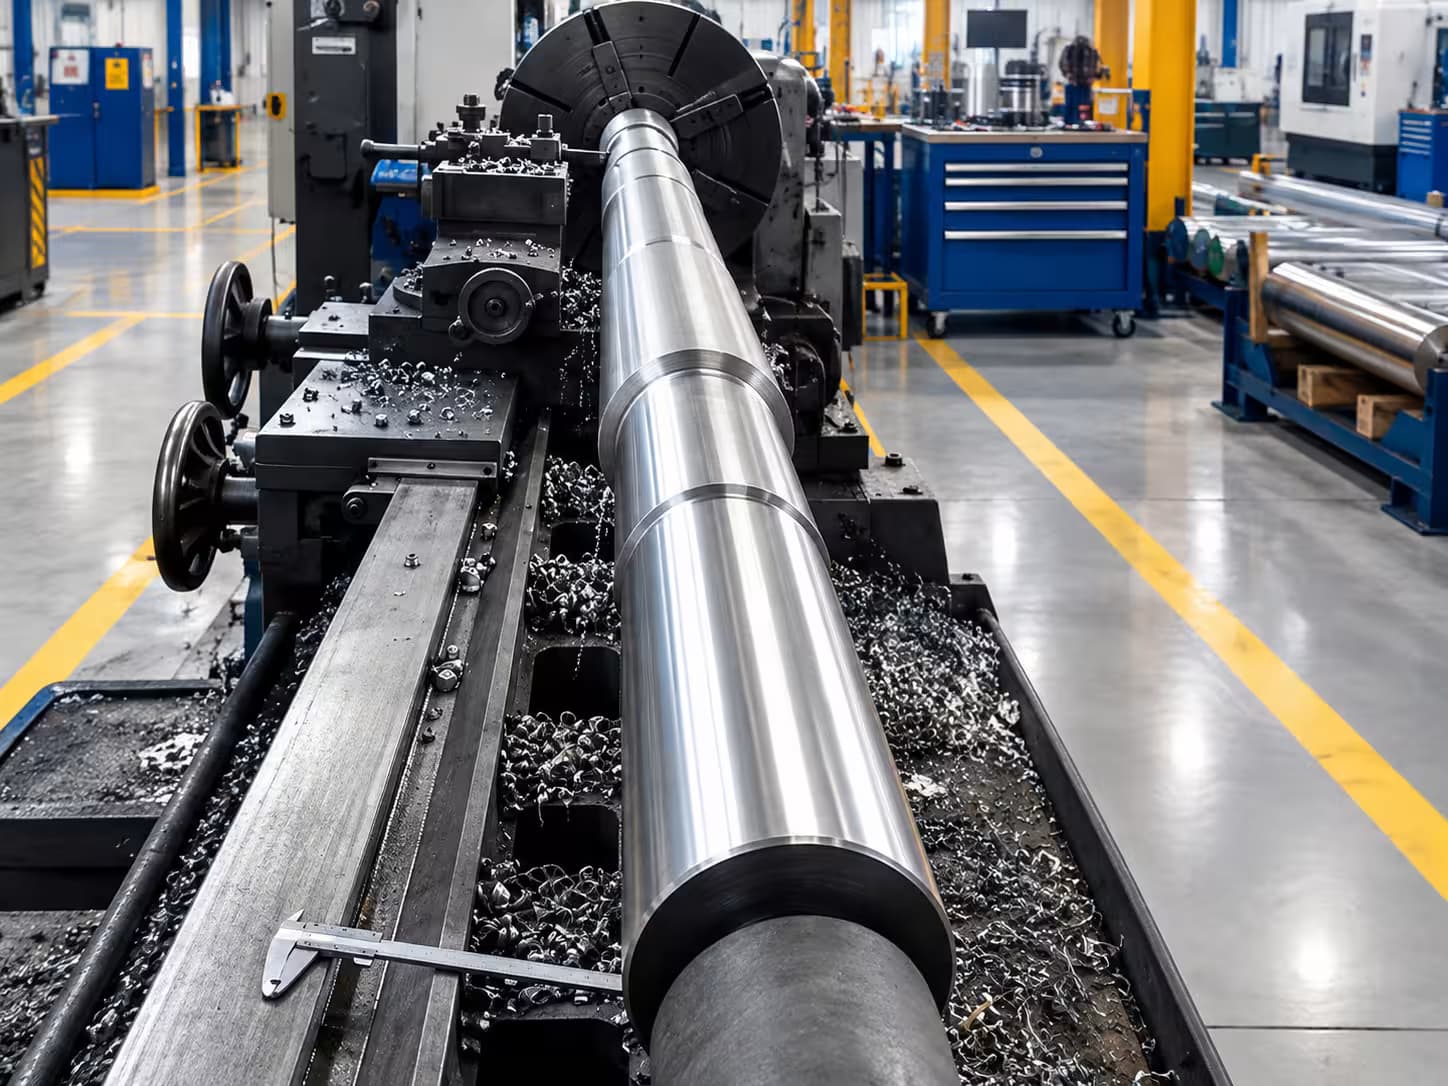
At an industrial heavy manufacturing and rotary process facility in Karachi, Alsons Hardware was contracted to execute the comprehensive hard chrome plating, journal reclamation, and precision cylindrical finish grinding of massive stepped drum shafts for heavy rotary drum spindles. Continuous high-torque rotation, abrasive industrial slurry exposure, and severe radial bearing loads had caused deep grooving, surface micro-pitting, and journal dimensional wear along the bearing seat areas, resulting in dangerous shaft runout and acute mechanical vibration across the drive train.
Our specialized machining and surface metallurgy division set up the multi-ton stepped drum shaft on heavy-duty engine lathes and cylindrical grinding rigs, skimming fatigued base metal to establish true concentricity and a uniform undercut profile. We immersed the journals in automated temperature-controlled chromium trioxide electroplating tanks, electro-depositing an engineered 60-micron dense micro-crack industrial hard chrome shell achieving a certified hardness of 65–68 HRC. The plated journals were subsequently precision ground and super-polished to Ra ≤ 0.15 µm mirror finish, returning bearing fits to strict DIN/ISO H7/h6 tolerances with zero measurable runout.
This drum spindle shaft reclamation project exemplifies Alsons Hardware's comprehensive industrial mechanical machining, hard chrome plating, and rotary equipment engineering services across Pakistan. Beyond drum shaft and spindle hard chroming, our specialized engineering workshops provide turnkey industrial solutions—including heavy lathe machining, dynamic rotor balancing, hydraulic ram re-chroming, thermal spray metalizing, bearing journal sleeved reclamation, and precision cylindrical grinding for sugar mills, cement kilns, steel re-rolling plants, paper manufacturing, and heavy process industries nationwide.
Client SectorIndustrial Rotary Drum & Mill Process Operators
Site LocationPrecision Machine Workshop & Hard Chrome Facility, Karachi
Turnaround10 Days Turnkey
HandoverCertified
TECHNICAL METROLOGY // AUDITED BENCHMARK
Technical Metrology & Quality
Engineering Properties & Standards
Calibrated mechanical tolerances, material benchmarks, and regulatory compliance standards verified on-site:
Shaft Geometry & Span
Stepped drum spindle shaft up to 4,500 mm span capacity
Plating Thickness Applied
60 µm (Microns) precision hard chromium layer
Surface Hardness Rating
65 – 68 HRC (Rockwell C Scale) hardness
Final Surface Roughness
Ra ≤ 0.15 µm mirror super-finish
Bearing Fit Standard
Precision DIN/ISO H7/h6 journal tolerances restored
Governing Standards & Codes
ISO 4526 Metallic Coatings — Electroplated Chromium • DIN EN ISO 6508-1 Hardness Testing • ASTM B117 Salt Spray Corrosion Testing
Diagnostic Analysis
Engineering Challenge & Deployed Resolution
Diagnostic failure mechanisms analyzed on-site and the turnkey engineered countermeasure deployed by Alsons Hardware.
ROTARY MILL SHUTDOWN HAZARDFAILURE MECHANISM
Journal Galling & Spindle Runout Defect
A heavy industrial rotary drum spindle shaft experienced severe bearing journal galling, deep 1.2mm radial score marks, and dimensional undersizing, causing excessive runout, bearing overheating, and mill operational stoppages.
•Deep axial scoring along drum shaft bearing seats causing severe radial play
•Excessive rotational runout and vibration risking catastrophic bearing seizure
•Imminent production line shutdown of heavy rotary drum processing unit
ALSONS PRECISION METALLURGYDEPLOYED RESOLUTION
Hard Chrome Electroplating & Precision Grinding
Executed precision lathe pre-machining and undercut grinding, electro-deposited 60 microns of high-density industrial micro-crack hard chrome at 65–68 HRC, and CNC cylindrical finish ground to Ra ≤ 0.15 µm mirror tolerance.
✓Heavy lathe setup and concentric undercut pre-grinding to true datum
✓Controlled 60 µm hard chromium electroplating achieving 65–68 HRC hardness
✓CNC cylindrical finish grinding and diamond super-polishing to Ra ≤ 0.15 µm
VERIFIED SITE OUTCOME:Bearing journals restored to zero runout with 100% bearing contact, eliminating mill vibration.
Engineering Sequence
4-Stage Execution Workflow & Milestones
Executed in strict accordance with Alsons Hardware industrial standard operating procedures and site safety protocols:
01
STAGE // 01METROLOGICAL AUDIT
Dimensional & Runout Laser Inspection
Inspected drum shaft using precision dial gauges and laser runout indicators to map journal wear, taper, and center concentricity.
Dimensional Ovality & Runout Inspection Certificate
02
STAGE // 02LATHE MACHINING
Heavy Lathe Skimming & Undercut Grinding
Machined damaged journals on heavy-duty engine lathe and cylindrical grinders, establishing a uniform, gouge-free undercut substrate.
Concentric Pre-Plating Undercut Verified
03
STAGE // 03ELECTRO-DEPOSITION
Micro-Crack Hard Chrome Deposition
Submerged drum shaft journals in automated chromium trioxide baths, depositing 60 microns of dense micro-crack hard chrome at 65–68 HRC.
60 µm Hard Chrome Plating Thickness Verified
04
STAGE // 04MIRROR POLISHING
Cylindrical Finish Grinding & Super-Polish
Ground journals to precise DIN/ISO H7 bearing fits and diamond super-polished to Ra ≤ 0.15 µm mirror finish with zero runout.
Zero-Runout Quality & Balance Certificate
On-Site Field Photography
Field Operations & Site Visual Records
High-resolution photographic documentation captured during turnkey field execution, specialized plant operations, and project delivery.
HEAVY LATHE MACHININGFIELD REF-01ARCHIVE LOG 01 // FIELD RECORD
Stepped Spindle Lathe Turning
Precision lathe pre-machining and skimming of worn bearing journals to establish true concentricity.
 DRUM SPINDLE PLATINGFIELD REF-02
ARCHIVE LOG 02 // FIELD RECORD
Thermal Spray & Hard Chrome Plating
Technicians applying industrial hard chrome and thermal barrier coatings to heavy drum spindle journals.
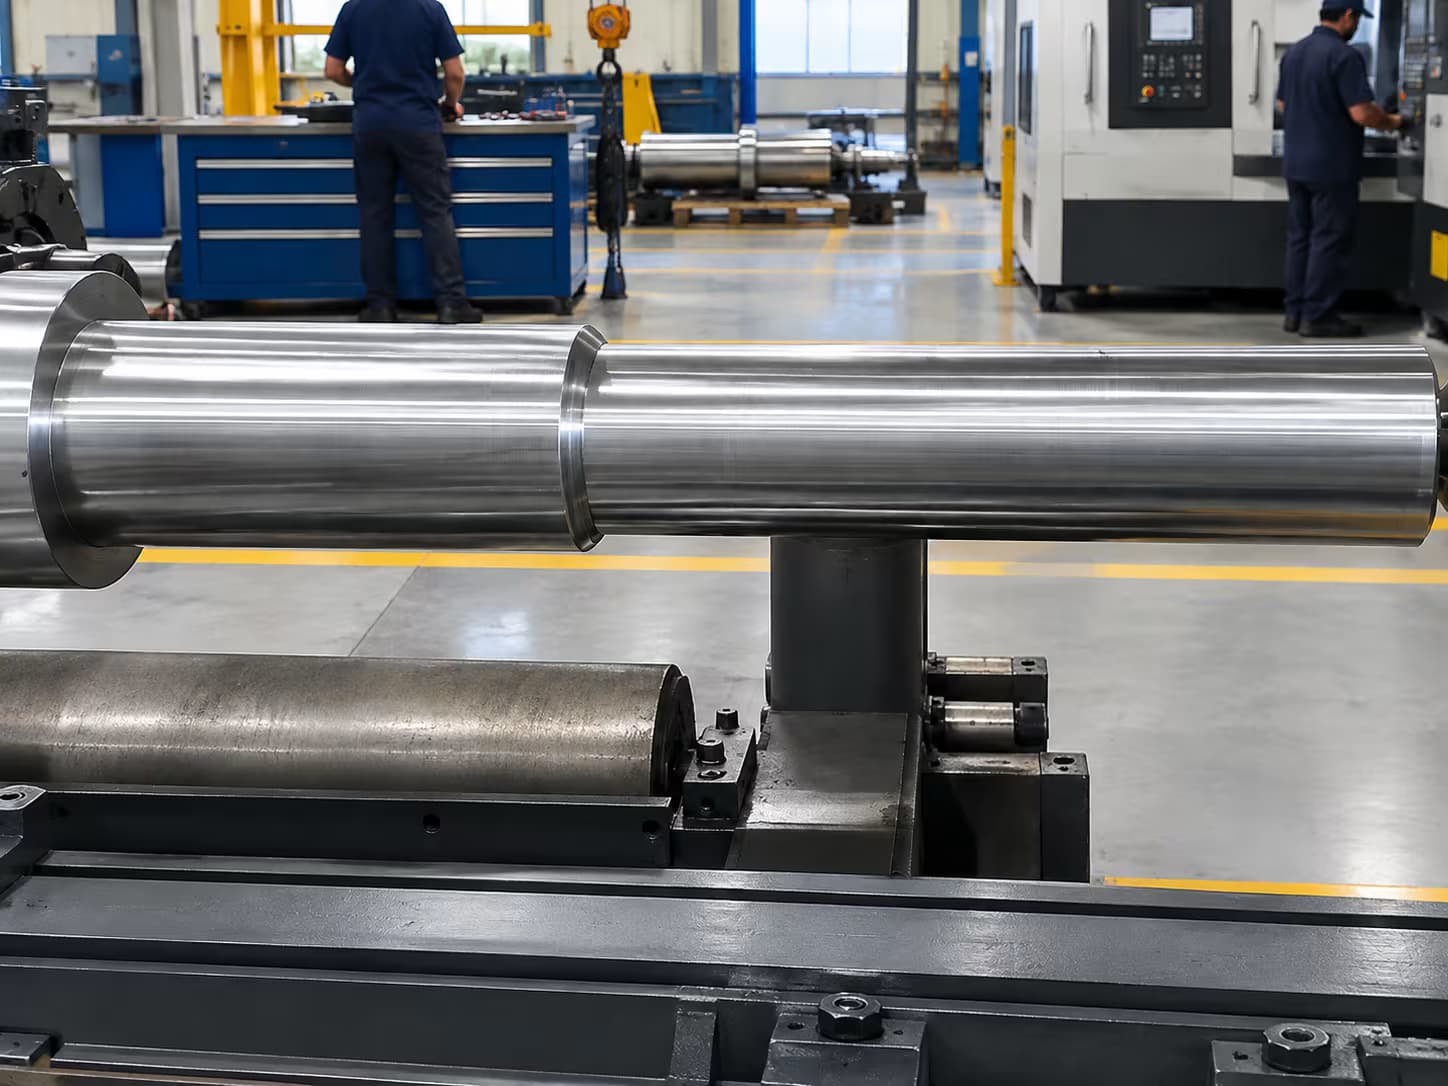 CYLINDRICAL FINISH QAFIELD REF-03
ARCHIVE LOG 03 // FIELD RECORD
Precision Cylindrical Finish Grinding
Sub-micron CNC finish grinding and diamond super-polishing to Ra ≤ 0.15 µm mirror tolerance.
Technical Advisory & FAQs
Frequently Asked Engineering Questions
Authoritative answers to common procurement, engineering standards, and execution queries regarding drum shaft chroming for drum spindle:
Why is hard chrome plating ideal for industrial drum spindle shaft reclamation?
Hard chrome plating deposits a low-friction, extremely wear-resistant layer (65–68 HRC) that restores undersized bearing journals to exact OEM tolerances without the thermal distortion associated with welding.
How does Alsons Hardware ensure concentricity and zero runout on heavy stepped drum shafts?
We mount multi-ton shafts between live centers on heavy-duty engine lathes and precision cylindrical grinders, using dial indicators and laser sensors to ensure TIR (Total Indicator Reading) runout within ±0.01 mm.
What is the surface finish roughness achieved after cylindrical grinding and polishing?
After precision finish grinding and multi-stage diamond paste super-polishing, our drum spindle journals achieve a mirror finish of Ra ≤ 0.15 µm, drastically minimizing bearing friction and heat buildup.
Industrial Portfolio
View All 7 ProjectsExplore More Engineering Projects
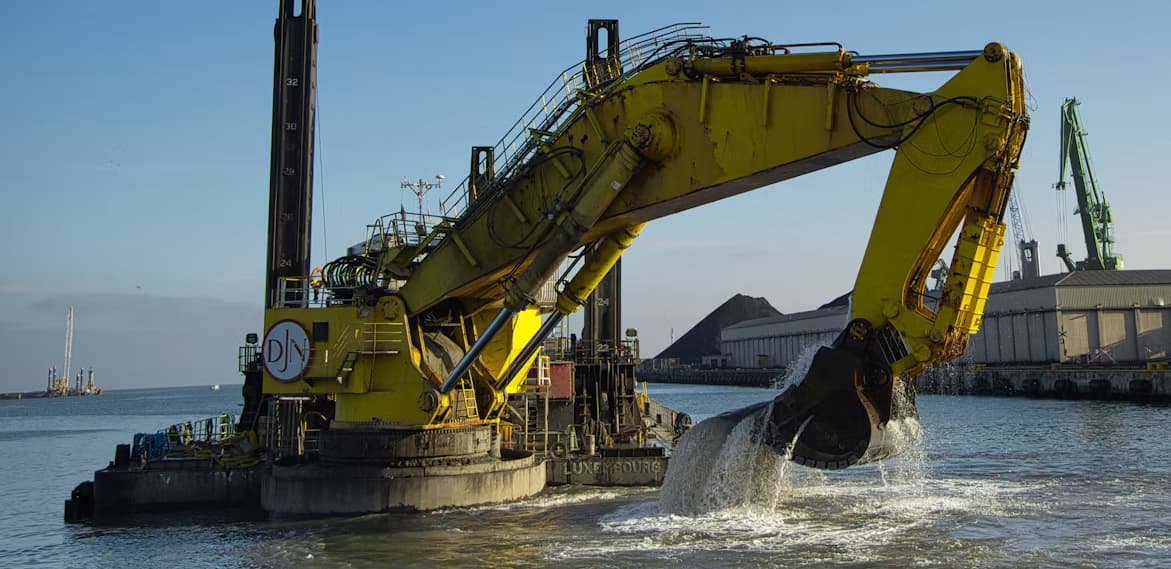 NAVAL INFRASTRUCTURE
Ormara Naval Base Dredging
Comprehensive underwater excavation, sediment extraction, and coastal navigation channel restoration executed under rigorous maritime security standards at Ormara Naval Base.
Case Study
 HIGHWAY INFRASTRUCTURE
Reflective Road Stud Installation
Precision road safety contracting delivering heavy-duty reflective cat eye road studs, engineered epoxy anchoring, and lane demarcation across industrial arterial routes.
Case Study
 MARINE BERTHING SAFETY
Marine Balloon Fender Installation
Supply, assembly, and precision rigging installation of heavy-duty pneumatic balloon fenders designed to absorb high-kinetic energy berthing impacts at active cargo jetties.
Case Study
 OFFSHORE BERTHING
Dolphin Fender Installation
Specialized installation of heavy cylindrical and cone rubber dolphin fenders onto offshore berthing piles designed to withstand extreme vessel contact during deep-sea mooring.
Case Study